When the weld looks right but the heat is moving
In high-frequency welding and hot-air or hot-wedge work, temperature drift is not always dramatic. The machine may still run, the operator may still see a bond forming, and the job may even pass a quick hand pull. The trouble is that the process is no longer sitting where it should, so seam width, gloss and edge definition begin to change over a shift.
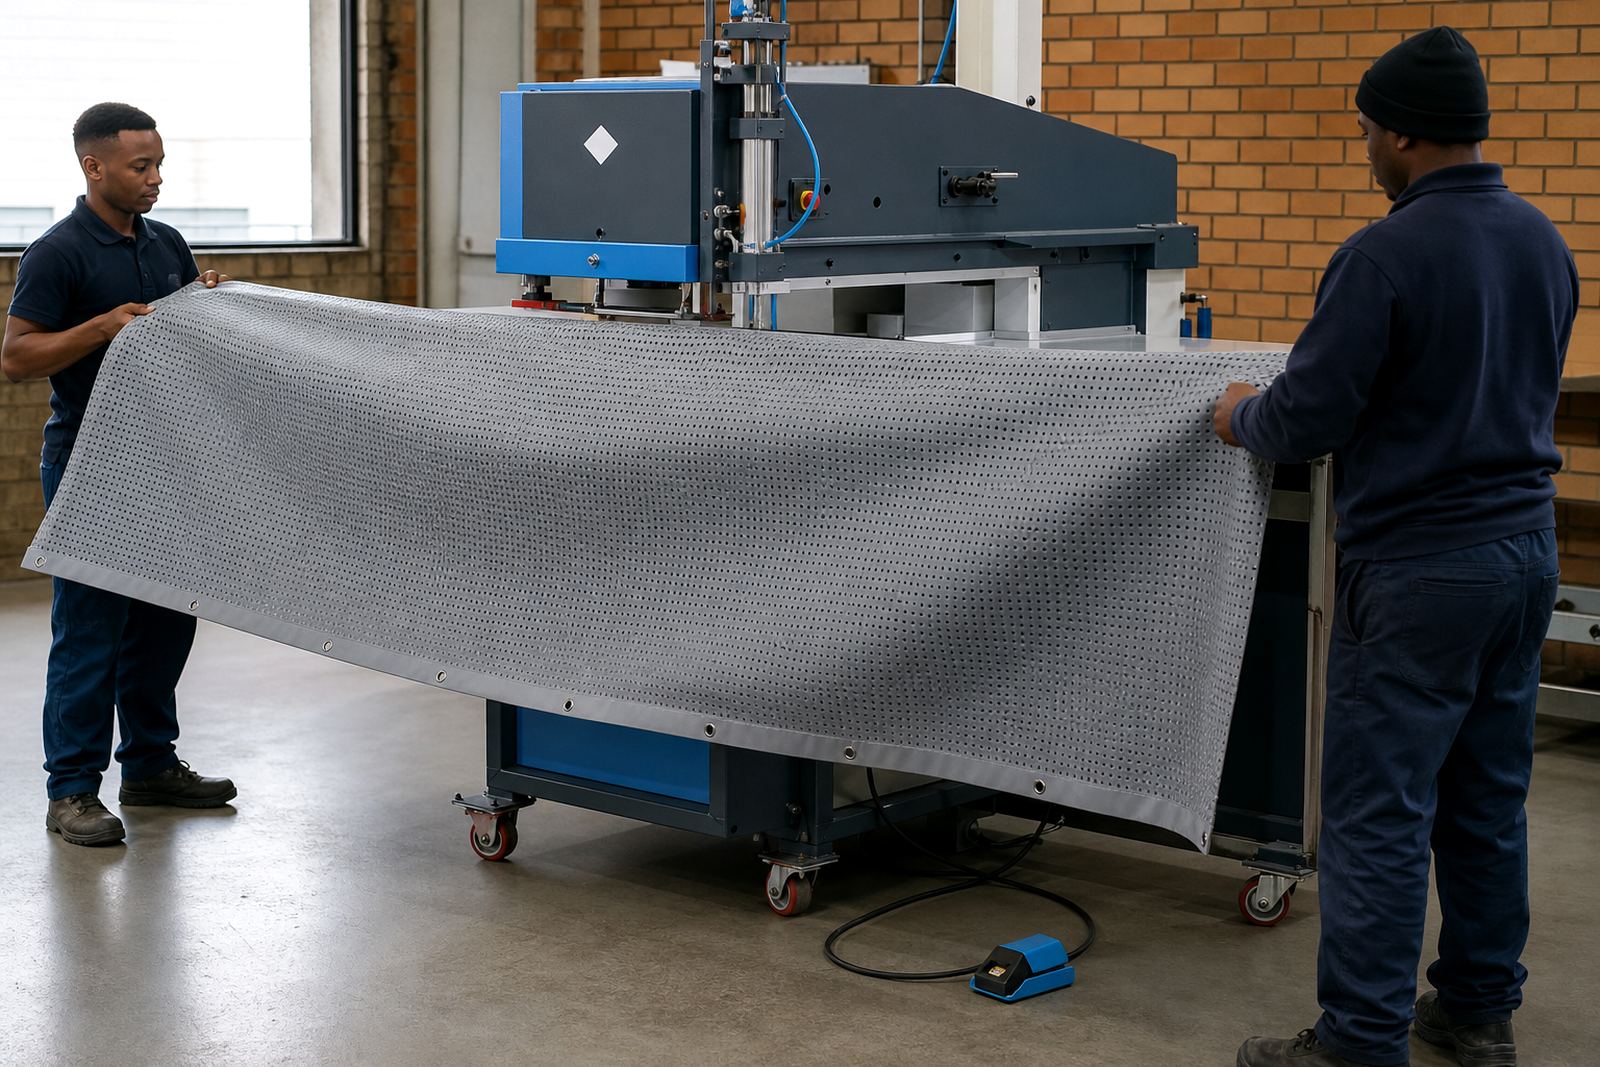
That matters on tarpaulins, banners and tent panels where the seam is expected to hold under tension and weather. A drift of only a small amount can alter the way PVC-coated fabric softens and flows, especially on longer runs where the operator is repeating the same weld all day.
What drift leaves behind on the finished panel
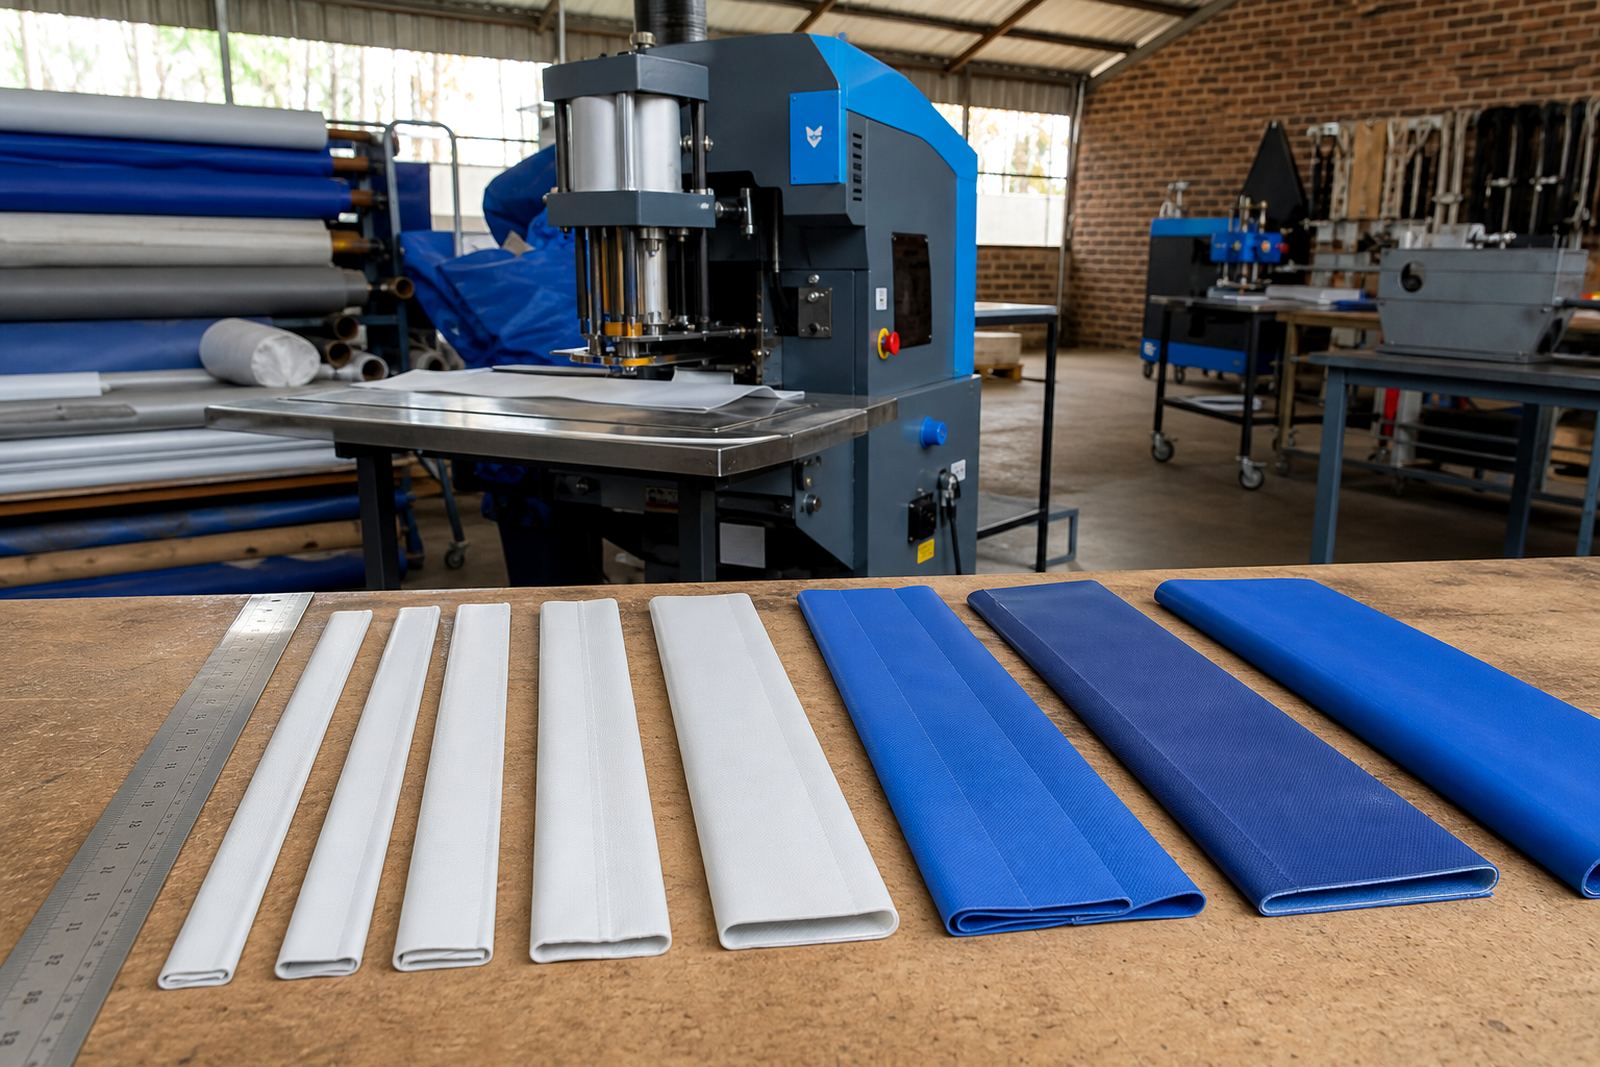
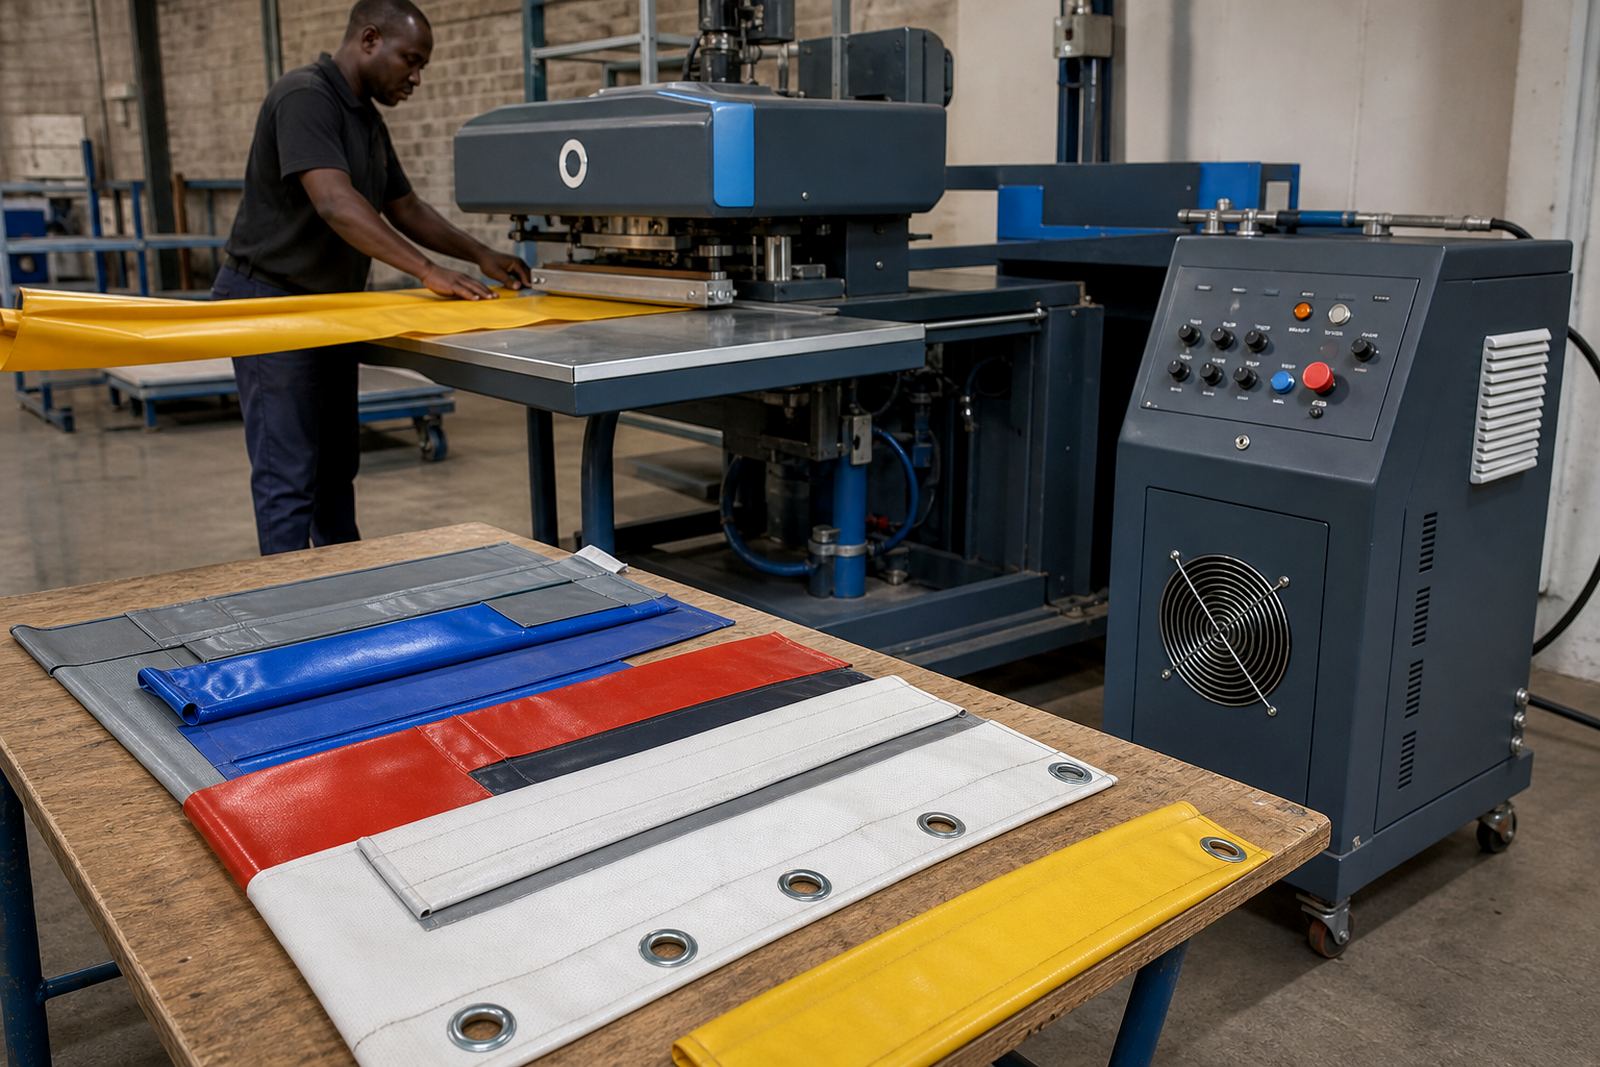
The first signs are usually visual. One section of a hem may look flatter than the next, or a keder pocket may sit a little uneven because the material was softer on one pass and stiffer on the next. In banner work, the edge finish can change from a neat, even line to a slightly shiny or wavy strip. On tent work, eyelet strips can start to show poor consistency if the base weld has shifted.
- Gloss changes along the seam
- Thin areas that feel harder or more brittle
- Extra puckering near hems or folds
- Uneven fusion on lap seams and reinforcement strips
- Bond failure at corners where heat was already marginal
When this happens, the issue is often blamed on the material, but the source is frequently the machine settings, electrode condition or poor heat transfer. Coastal humidity in Durban can make operators think the PVC is behaving differently, yet the real fault may be a temperature setting that is drifting through the day.
Why high-frequency and hot-air systems drift differently
High-frequency welding depends on controlled energy delivery into the PVC layer. If the output is not stable, the weld zone may change from one cycle to the next even when the setting on the panel looks unchanged. Hot-air and hot-wedge machines behave differently because airflow, element condition and roller pressure all affect the actual temperature reaching the fabric. The set point is only part of the story.
Common causes include worn elements, dirty air paths, tired rollers, poor tooling alignment and unstable mains supply. In workshops across Germiston, Johannesburg and Pretoria, it is not unusual to see drift caused by service items that were put off for too long. On a hot afternoon in Bloemfontein, heat build-up around the machine can also change the way the weld zone behaves, especialy on long production runs.
- Airflow restriction in hot-air units
- Worn or pitted electrodes on high-frequency machines
- Incorrect pressure on wedges, rollers or guides
- Loose fittings or poor machine alignment
- Power fluctuation during peak workshop loading
The operator checks that catch drift early
An operator does not need to be a technician to spot a drift problem. A steady routine at the start of a shift helps. Check the seam sample, compare both sides of the weld, and watch for colour shift, edge lift or a change in the way the fabric feeds. If the machine needed more time than usual to reach a stable weld, that is worth recording too.
For workshops doing hems, keder work and eyelet strips on the same day, consistency checks need to happen between job types. A machine set for a heavy tent seam may leave a lighter banner hem too hot, while a setting trimmed for thin material may under-weld a reinforced pocket. Keep a sample piece from the same batch nearby so you can compare the finish before production gets too far along.
- Run a short test seam before full production
- Check both the front and back of the weld
- Look for changes after a break or tool change
- Record settings for each material thickness
- Pause if the seam starts looking brighter or softer than expected
Servicing that keeps the heat where it belongs
Preventive servicing is the most practical way to limit drift. Electrode refurbishment, roller replacement and tooling alignment all help keep the heat and pressure where the seam needs it. On hot-air and hot-wedge equipment, cleaning the air passages and checking the heating elements reduces the chance of a slow shift in performance. On high-frequency units, electrode condition and contact pressure need regular attention because small wear patterns can become a repeat fault.
Site callouts are useful when a workshop keeps seeing the same defect on different jobs. A technician can test the machine under load, inspect the seam quality and look at the full setup instead of just the symptom. In Germiston, where many tarpaulin makers are running back-to-back production, a machine that drifts half a setting across a shift can waste fabric and create rework that nobody wants.
A Germiston case with a Durban-style finish problem
A banner and tent maker in the Ekurhuleni area had one recurring complaint: the first metres of a job looked perfect, but by the afternoon the seam finish was changing and the edges were showing a slight shine. The team assumed the PVC batch was inconsistent. After a service visit, the issue traced back to a heater control that was no longer holding its range properly, along with a roller that had started to wear unevenly. Once those parts were corrected and the operator retrained on sample checks, the finish settled back to normal.
The lesson was straightforward. Temperature drift is not only a machine issue, and it is not always obvious on the first panel. It shows up in the seam, in the finish and in the time spent fixing work that should have been right the first time.